Search

Hongke's latest articles

HongKe

Add your title text here

I. Introduction: Strategic Changes at the Data Layer under the Critical Infrastructure Legislation

Add your title text here

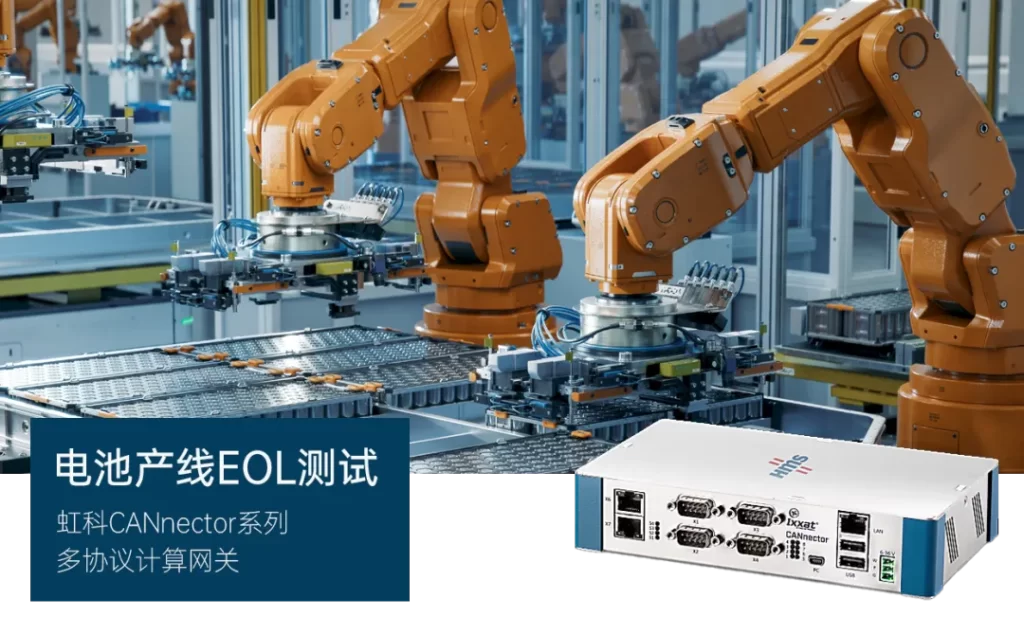
[Hongke Solutions] Tight production line cycle times? Hongke CANnector enables efficient battery system testing with its DoIP gateway capabilities.

What Are the Cycle Time Bottlenecks in New Energy Battery Production Lines and the Transition to DoIP?

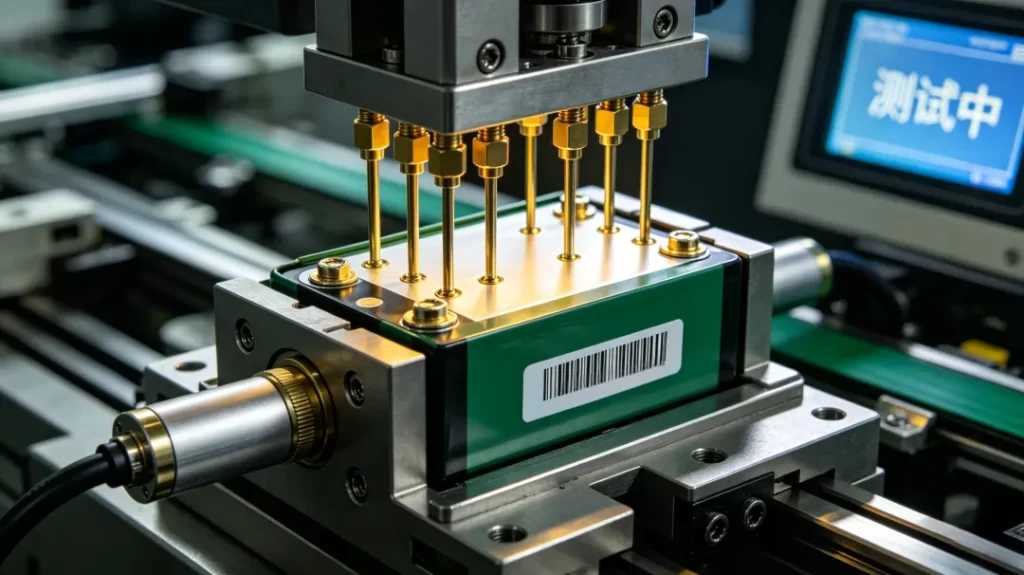
With the explosive growth in production capacity demand for electric vehicles (EVs), battery system (BMS/Battery Pack) manufacturing lines now require cycle times with precision down to the second. During end-of-line (EOL) testing and functional validation, test equipment must perform extensive parameter readings, diagnostic trouble code (DTC) diagnostics, safety logic calibration, and firmware updates (FOTA/EOL Flash) on the battery packs.

However, traditional diagnostic architectures based primarily on CAN/CAN FD buses are facing serious bandwidth bottlenecks. Due to CAN FD’s limited transmission rates and load capacity, traditional interfaces often result in excessively long programming times and accumulated test bottlenecks when dealing with battery management firmware—which frequently runs into the hundreds of megabytes (MB)—and high-frequency data acquisition, thereby prolonging the cycle time of the entire production line. To overcome this bottleneck, an Ethernet-based DoIP (Diagnostics over IP, ISO 13400) The protocol has become the standard choice for E/E architecture and production line testing of the new generation of new energy vehicles.

以DoIP網關為核心,虹科CANnector系列設備透過延遲最小化的協定轉換、獨立運行的硬體架構、以及一體化的測試平台能力,幫助客戶在電池 ECU 快閃記憶體環節實現了20%的效率躍升。

Three Major Efficiency and Data Challenges Faced in Battery System Production Line Testing

1. Insufficient bandwidth on the traditional CAN bus causes delays in programming and diagnostics

In battery pack EOL testing, firmware flashing and the parallel reading of status data from multiple battery cells require extremely high throughput. Traditional CAN buses have a maximum speed of only 1 Mbps, and even CAN FD struggles to handle the instantaneous transmission of large volumes of data, resulting in persistently long test times for individual battery packs and directly reducing production line throughput.

2. Delays in Multi-Bus Protocol Conversion and the Risk of Data Loss

Modern battery systems incorporate a variety of communication protocols, including CAN, CAN FD, LIN, and in-vehicle Ethernet. If a test gateway lacks high-performance hardware routing and data buffering capabilities, data packet delays or even packet loss can easily occur during heterogeneous network data forwarding and DoIP protocol conversion, leading to misinterpreted test results and the need for retesting.

3. Complexity and Flexibility Requirements for Automated Test Environments on Production Lines

Automated production lines place extremely stringent demands on the stability and interface expandability of test equipment. Test gateways must not only support DoIP diagnostics but also integrate flexibly with existing PLCs, host-based test software (such as LabVIEW and the Vector toolchain), and MES systems; otherwise, system integration and maintenance costs will increase significantly.

The Heavy Price Battery Manufacturers Pay for Production Line Efficiency Losses

In the highly competitive new energy vehicle market, even minor delays in test cycle time can add up to create significant financial and operational pressure for companies. When the testing phase on the production line is delayed due toDiagnosed as lag caused by insufficient bandwidth... The most direct impact is that overall throughput is constrained, leading toDecreased equipment utilization...and was unable to deliver the high-value battery pack order on time.

The deeper cost lies in the loss of control over product quality and operating costs. In an effort to keep up with the demanding production line pace, if companies choose to reduce testing procedures or lower data collection frequency, they run a high risk of creating potential quality issues. This can result in defective products entering subsequent assembly stages or the end market, ultimately leading to costly recalls and damage to the brand’s reputation.

In addition, frequent test timeouts and protocol translation errors can increase unplanned downtime on automated production lines. On-site engineers must spend a significant amount of time debugging and manually retesting, which not only drives up labor and operating costs but also causes companies to lose their competitive edge in the transition to automation and digital transformation.

Hongke CANnector Solution: Redefining High-Efficiency Battery Testing with DoIP Gateway Capabilities

To resolve production line cycle time bottlenecks and ensure high-quality battery system testing, companies must upgrade to a high-bandwidth, flexible, and reliable gateway architecture.Hongke CANnector Smart Multi-Channel GatewayDesigned specifically for testing new energy vehicles and battery production lines, it enables efficient testing with powerful DoIP gateway capabilities:

1. Ultra-fast DoIP diagnostics and high-capacity programming capabilities

Hongke CANnector provides full support ISO 13400 (DoIP) Compliant with industry standards, it provides 100 Mbps/1 Gbps in-vehicle Ethernet interfaces. Thanks to Ethernet’s high-speed data transmission, the time required for battery pack firmware updates and diagnostics is reduced by several times, significantly shortening the test cycle time per unit.

2. Multi-Protocol Heterogeneous Routing and Zero-Packet-Loss Hardware Architecture

CANnector integrates multi-channel CAN FD, LIN, and Ethernet interfaces and features powerful hardware routing and data processing capabilities. It enables low-latency, seamless translation between CAN and DoIP, as well as between CAN FD and Ethernet, ensuring data integrity even under heavy test loads.

3. Flexible hardware and software integration and support for production line automation

It offers modular interface configuration and a comprehensive API SDK, supporting seamless integration with production line HMI software and MES systems. Engineers can easily define custom routing logic and diagnostic commands to accommodate the diverse testing requirements of battery packs.

Hongke CANnector Key Advantages

「虹科CANnector系列」在此場景中被用作DoIP網關,結合診斷測試軟體,建構了高效通訊鏈路:

1. Multi-Protocol Integration

Multiple Channels Integrated into a Single Device CAN / CAN FD / LIN / In-Vehicle Ethernetand digital I/O, perfectly meeting the multi-bus interconnection requirements of complex automotive electronics and industrial automation.

2. Embedded Standalone Operation

Applications run natively on a Linux platform. The PC is only needed for initial setup; once downloaded, the applications can run independently and stably without the PC, significantly reducing the risk of system crashes.

3. Rigorous Industrial-Grade Reliability

With the highest 2 kV DC Interface Isolation ProtectionSupport -40°C to 80°C Wide-temperature operation and DIN rail mounting, designed specifically for harsh industrial and production line environments.

4. Drag-and-Drop Configuration (Effortless Configuration)

Through ACT The software features a minimalist drag-and-drop logic configuration and supports ARXML file import, significantly shortening the deployment and go-live cycles for automated production lines.

5. Flexible Software Integration

We offer a free ECI driver package that natively supports Linux, QNX, and ARM/x86 architectures, enabling seamless integration into customers' existing automation and production line test systems.

Frequently Asked Questions

Q1: What is a DoIP gateway? Why does EOL testing for battery packs require DoIP capability?

A1: DoIP (Diagnostics over IP, ISO 13400) is an in-vehicle diagnostic technology based on the TCP/IP protocol. Battery pack EOL testing requires the transmission of large amounts of BMS firmware and high-frequency data, for which the traditional CAN bus lacks sufficient bandwidth; however, the Hongke CANnector, equipped with DoIP gateway capabilities, provides high-bandwidth transmission, significantly reducing diagnostic and flashing times.

Q2: How does Hongke CANnector help battery manufacturers reduce cycle time on their production lines?

A2: Hongke CANnector efficiently converts traditional CAN/CAN FD diagnostic data into the Ethernet DoIP protocol, utilizing bandwidths of up to 100/1000 Mbps for parallel data transmission and rapid programming, thereby shortening the test cycle for individual battery packs, thereby improving overall production line throughput and capacity.

Want to learn more about how to optimize your battery production line testing processes using an enhanced data gateway and DoIP technology? Visit us nowHongke CAN / CAN FD / LIN Bus SeriesLearn more on the product page.

Other Articles

Hongke Case

[Hongke Applications] Hongke IDS Multi-Camera Imaging Solution – Overcoming the Challenge of Precise 3D Observation of High-Speed Dynamic Plasma

Hongke, in collaboration with IDS, offers a multi-camera synchronized imaging solution featuring microsecond-level ultra-short exposure and back-illuminated global shutter CMOS sensors, successfully overcoming bottlenecks in high-speed, microscale plasma 3D point cloud reconstruction and dynamic observation. Learn more about Hongke’s industrial machine vision solutions today!

Read more
Hongke Case

[Hongke Case Study] Panorama Essentials: A Lightweight SCADA Solution—An Industrial Monitoring System with Unlimited Web Users and Low Cost

Hongke has officially launched Panorama Essentials, a lightweight SCADA solution designed specifically for small- and medium-sized industrial monitoring and building automation. With support for unlimited web user connections, up to 25,000 data tags, and “Cyber-by-design” native cybersecurity, it significantly reduces system deployment costs and engineering commissioning time. Learn more about this professional-grade SCADA upgrade solution today!

Read more
Hongke Dry Goods

[Hongke Solutions] Pharmaceutical Warehouse Mapping Validation and EMS Monitoring Solutions – Hongke ELPRO Meets WHO & GDP Standards

Hongke ELPRO provides professional temperature distribution validation (mapping) for pharmaceutical warehouses and EMS solutions for continuous, automated monitoring of temperature and humidity. We successfully assisted the apo.com Group in completing mapping validation for its Autostore automated high-bay warehouse within two months. The 100% system complies with WHO Annex 9, EU GDP, and GxP standards, ensuring the safety of the pharmaceutical supply chain and enabling the company to successfully pass regulatory audits.

Read more

Contact Hongke to help you solve your problems.

Let's have a chat